Why Most Vision Systems See in Black and White
Walk past an inspection station on a production line and there's a good chance the camera checking the product only sees in shades of grey. That surprises people, especially when the product itself is brightly coloured. But for most inspection jobs, a black and white (monochrome) camera is the better choice. Here's why, and when colour is worth it.
How a colour camera works
Most colour cameras use a single sensor with a pattern of tiny red, green and blue filters laid over it. Each pixel only measures one of those three colours, and the camera works out the full colour of every pixel by looking at its neighbours.
That works well for photographs, but it has a cost. Because each pixel is only measuring part of the picture, some fine detail is lost, and the filters block some of the light before it ever reaches the sensor.
Why mono usually wins
A monochrome camera has no colour filter, so every pixel measures the full amount of light falling on it. That gives two practical advantages.
Sharper detail. Every pixel contributes real information, so edges are crisper and small features are easier to measure. On a job where the smallest defect only covers a few pixels, that matters.
More light. Without the filter, more light reaches the sensor. That means shorter exposure times, which is what you need when parts are moving quickly and any blur would hide the detail you're looking for.
Finding colour without a colour camera
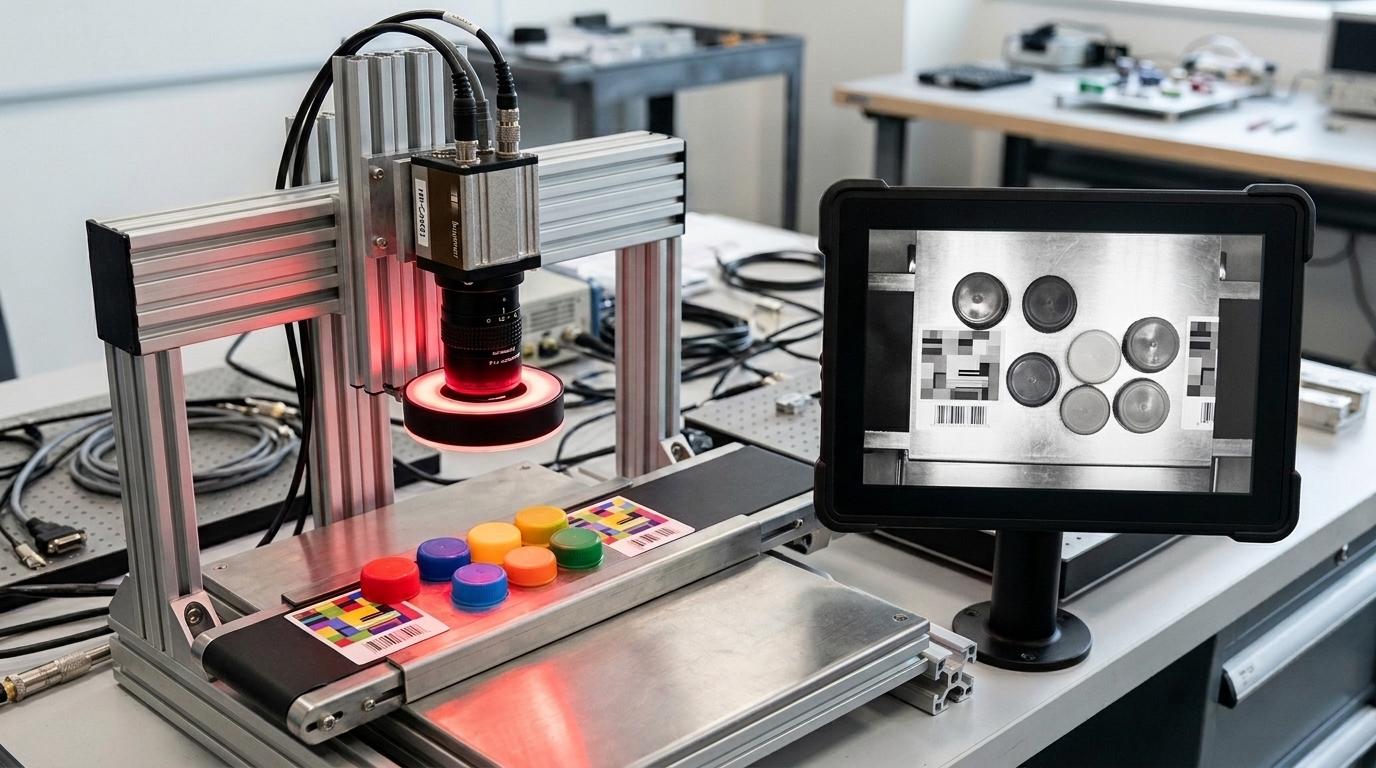
Even when a feature is defined by colour, you can often pick it out with a mono camera by choosing the colour of the lighting carefully. Light of a particular colour makes surfaces of a similar colour look bright and opposite colours look dark. With the right choice of light, a feature can stand out sharply against its background, or a distracting pattern can fade away.
That's why we'll often pair coloured lighting with a mono camera. It gets you the sharpness and light of a mono sensor while still bringing out what matters most in machine vision, which is contrast. A camera doesn't need to know what colour something is to inspect it. It needs the feature to stand out clearly from everything around it, and the right colour of light is often the easiest way to make that happen.
It's one of the reasons lighting is such a big part of designing any vision system.
When colour is the right tool
Colour cameras earn their place when the colour itself is what's being checked. Making sure the right coloured cap goes on the right bottle, checking print matches its approved artwork, or sorting parts by colour are all jobs where a mono camera would struggle, however well it was lit.
In those cases we'll specify colour, and design the lighting and optics to get the most out of it.
Choosing the right camera for the job
Like every other part of a vision system, the camera choice comes from the job, not the catalogue. Because we're independent of any single manufacturer, we can choose the sensor, lens and lighting that suit your parts and your line, whether that's mono, colour, or a mix of both.
If you're not sure what your application needs, send us some samples. Our engineers can test them in our lab and tell you which setup will give you reliable results.
Call us on +44 (0) 1933 62 51 62, email info@fishersmith.co.uk, or book a call with an engineer at www.fishersmith.co.uk.